
Knowing how to manage overseas manufacturing projects starts with comparing total landed cost, not just the factory quote. Include tooling, freight, tariffs and duties, insurance, management time, and the cost of correcting problems. Weigh those expenses against product quality, delivery risks, and the controls needed to protect your intellectual property.
Lower production costs can make overseas manufacturing attractive, but savings depend on the product, order volume, materials, processes, and destination market. A competitive unit price will not help if unclear specifications, inconsistent production, or delays undermine the final result.
This article explains how to assess benefits and risks, build a complete cost comparison, and set quality expectations before production begins. It also covers practical safeguards for designs and licensed artwork, from approved samples and clear specifications to production oversight and inspections. The aim is to make a better-informed sourcing decision and avoid surprises between the factory quote and finished goods arriving at your warehouse.
• Match the manufacturing country and supplier to your product’s materials, processes, order volume, destination market, and risk profile.
• Compare landed cost per unit, accounting for more than the factory quote, including freight, duties, tooling, and project management.
• Set quality expectations through clear specifications and an approved sample, then use inspections at relevant production stages.
• Protect designs and licensed artwork with appropriate legal agreements, controlled access to files, and clear approval processes.
• Compare labor rates alongside productivity, quality controls, logistics, and the total cost of delivering acceptable goods.
Overseas production can improve costs, capacity, or access to materials, but a factory quote alone cannot show whether it suits your product. Start by mapping the product’s processes, expected volume, destination market, delivery requirements, and supply-chain risks. Then weigh those needs against supplier capability, production controls, logistics, and the full cost of bringing acceptable goods to market.
How does a professional evaluate and select an overseas manufacturer or contract manufacturer? They compare factories by process, material, part size, tolerance, volume, capacity, and quality systems. They also assess whether a factory can meet the approved specification, manage changes, communicate problems, and support the required production schedule. A factory audit and sample review help test its operational claims against actual processes.
Country selection follows the same product-specific logic. China, Vietnam, India, and Thailand may be considered in a China-plus-one strategy, while Mexico may suit some North American supply chains. The right location depends on production capability, order size, destination, shipping route, tariff exposure, and suitable supplier availability. A detailed figurine, for example, requires different process expertise than a simple printed card game. The country name alone does not establish whether a factory is a good fit.
Overseas manufacturing may be less suitable when production volume is small, specialized domestic requirements dominate, or the delivery plan cannot absorb longer logistics and coordination. Assess vulnerabilities such as reliance on one supplier, material shortages, manufacturing-country holidays, customs delays, and port disruption. Backup suppliers, contingency plans, and flexible logistics can reduce exposure, but each option changes project costs and management needs.
What labor, environmental, and product compliance rules apply in major overseas manufacturing countries? Requirements depend on the manufacturing country, destination market, product type, and intended use. They are not uniform across China, Vietnam, India, Thailand, and Mexico. Review product safety, environmental controls, and labor practices for the specific country and product before committing to production.
The OEM should retain ownership of the functional specification, approved design, and release decisions. Before production starts, the production package should define drawings, tolerances, materials, finishes, packaging, and an inspection plan. For a multi-component board game, that means documenting component counts, artwork versions, assembly, and acceptable print variation. An approved sample gives production teams a physical reference, while in-process checks can identify deviations before final inspection.
A local manufacturing partner coordinates factory communication, engineering alignment, production follow-up, and logistics documentation. Customs processes and transport channels affect delivery timing, so the partner tracks these alongside production milestones. For teams seeking OEM and ODM contract manufacturing support, coordinated oversight connects specifications, factory execution, and shipment planning without transferring product-release authority away from the OEM.
Compare manufacturing options by landed cost per sellable unit at the destination warehouse, not by factory quote alone. A practical model adds unit price, tooling, fixtures, line setup, freight, duties, insurance, compliance audits, management time, travel, and problem correction. Divide the total by the quantity expected to arrive in acceptable condition. This reveals expenses a low unit quote can conceal, including costs incurred before production or after a quality issue.
Separate one-time and recurring expenses. Tooling and fixtures may require upfront investment, while production units, packaging, and transport recur with each order. Higher volume can spread tooling costs across more units, but it also increases inventory commitments and exposure if the design changes. Compare expected order quantities and include samples, setup work, rejects, and replacement production where applicable.
Overseas manufacturing may cost less because of lower labor expenses, access to raw materials, established production infrastructure, or available factory capacity. The advantage depends on the process and product, not simply the country. For a plastic injection-moulded item, tooling and material choices can shift costs between setup and each unit. Compare equivalent specifications and quality expectations to avoid misleading quote comparisons.
Freight and customs also affect the result. The estimate should identify transport mode, shipment dimensions and weight, insurance, handling, inland delivery, customs fees, duties, and responsibility for import formalities. Transit time depends on the route, transport mode, port handling, inland movement, and shipment conditions. Keep the production schedule separate from transport estimates, then allow for handoffs and potential disruptions in the overall delivery plan.
What are typical costs and timelines for setting up overseas manufacturing? Costs depend on product complexity, tooling, order volume, freight, duties, and oversight. The schedule follows supplier selection, development, sampling, production readiness, manufacturing, and delivery. Each stage depends on the product and factory plan.
A sourcing and procurement partner builds a quote from defined product requirements, quantity, packaging, destination, and delivery terms. A useful breakdown separates factory charges from logistics and import costs, states its assumptions, and identifies items that may change. Product classification, origin, customs value, documents, and importer responsibilities shape the customs estimate. Assess tariff exposure for each manufacturing country and revisit it when schedules or sourcing conditions change.
Make supplier estimates comparable by aligning product revision, order quantity, packaging, inspection scope, and named delivery point. Request separate cost lines for tooling, unit price, freight, duties, and management. This makes the trade-offs visible and gives project teams a consistent basis for decisions. A reliable landed-cost estimate depends on current shipment details and a clearly defined commercial arrangement. Discuss a project-specific cost breakdown.
A professional manages factory quality control through defined checkpoints, documented acceptance criteria, and corrective-action follow-up. The plan starts before production, then checks materials, early output, production progress, and finished goods before shipment. Each checkpoint targets a known risk, such as paint consistency on a figurine or correct component counts in a board game. This sequence helps teams address process problems before they affect a larger batch.
The golden sample turns design intent into a physical production reference. It should represent the approved materials, dimensions, colours, decoration, assembly, and packaging, with its revision and approval recorded. Keep two copies of the approved physical sample, one at your office and one at the factory. If artwork or a material changes, document the revision and affected production batch before work continues. Inspectors can then compare production output with the same approved reference.
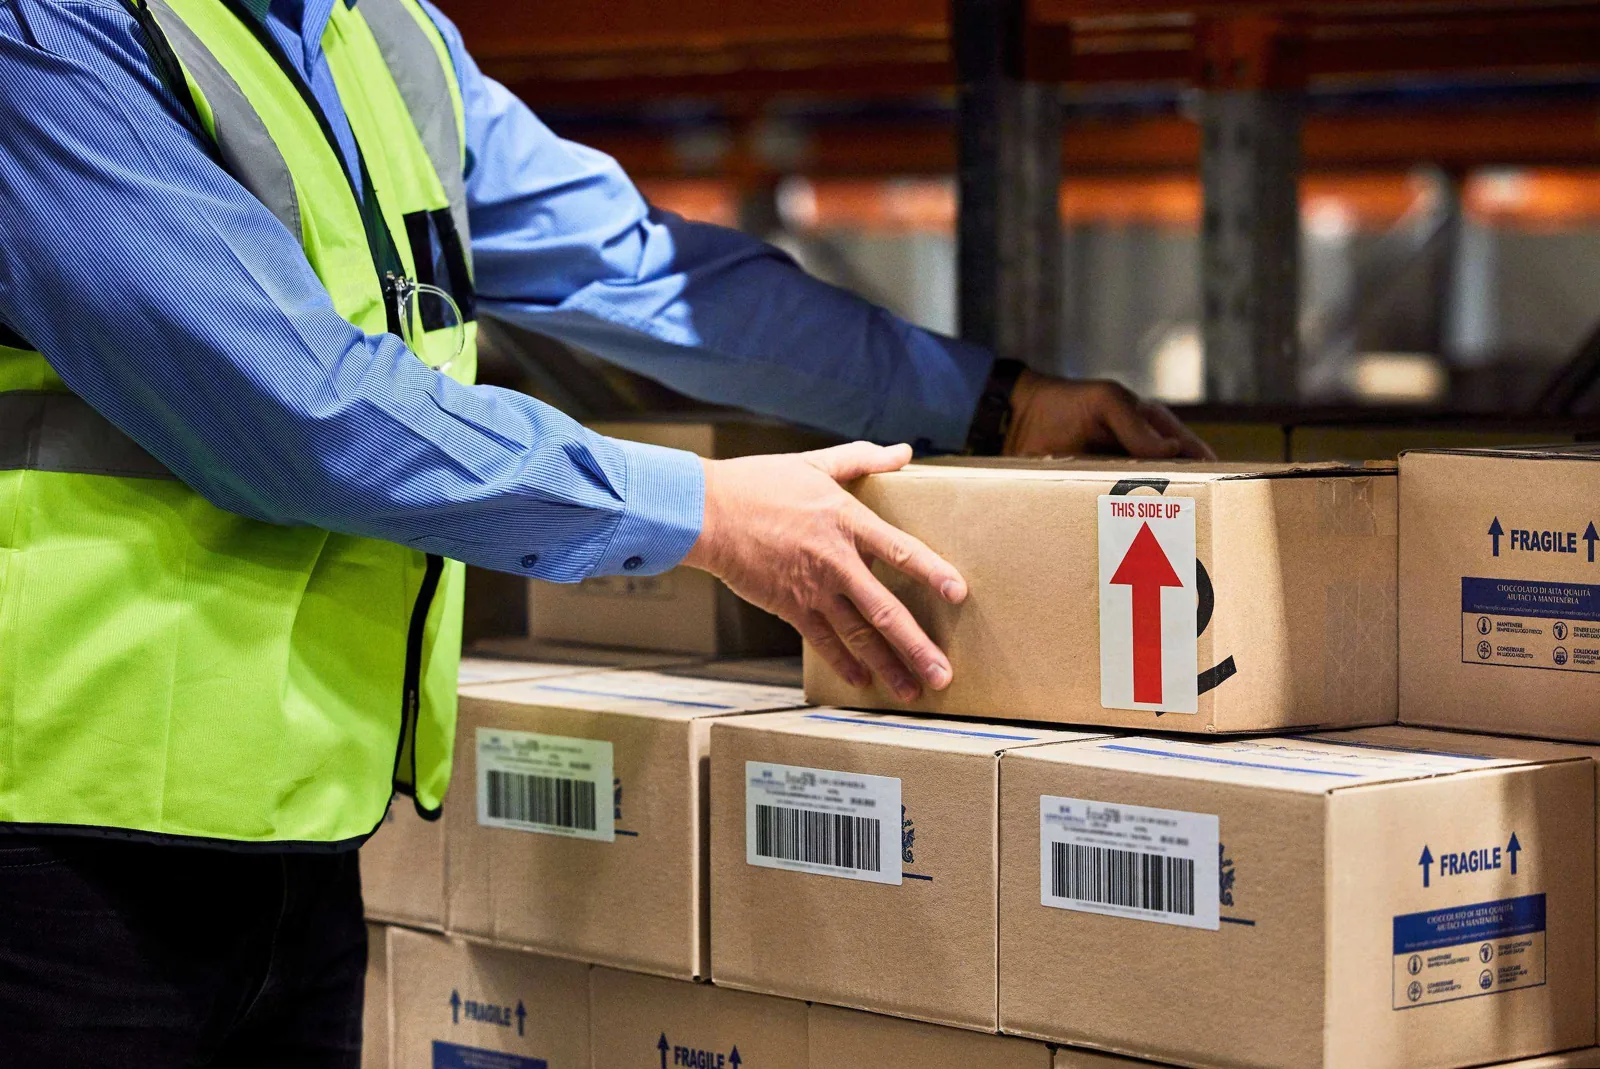
How does a professional manage quality control and inspections at overseas factories? They translate specifications into a checklist, arrange checks during production and before shipment, and report findings with photographs and measurements. For a multi-component product, the record can capture component counts, assembly, packaging, and functional checks against agreed criteria. It should also identify the sample or units inspected so findings remain traceable.
A team’s factory presence gives it direct visibility into production conditions, while a third-party inspection provides an independent snapshot against the agreed standard. A quality plan should identify critical characteristics, defect categories, severity, sampling approach, and evidence required for each check. AQL sampling can structure a final random inspection, but it does not guarantee that every unit is defect-free. Inspection results need clear acceptance criteria and a documented response to failures.
When inspectors find a defect, the report should identify the affected item or batch, show evidence, and describe the required correction. The factory then records the root cause, containment action, rework or replacement decision, and verification result. Production follow-up matters because a final inspection can reveal a problem without recovering time already lost. A corrective-action log keeps owners, decisions, and closure evidence visible across the project.
How do time zones, language, and cultural differences affect project management with overseas manufacturers? Time-zone gaps can delay clarification when questions reach the factory after local working hours. Unclear terminology can also lead to different interpretations of tolerances or defects. Bilingual quality-control documents reduce this risk by pairing consistent terms, annotated images, units, sample references, and approval records in both working languages.
Communication should name a decision owner, response deadline, and escalation route for each quality issue. For example, pause an artwork mismatch, photograph it, compare it with the approved file, and release it only after the designated owner records a decision. This process connects factory reporting with corrective action rather than leaving inspection findings as isolated paperwork. A shared issue log also makes unresolved decisions visible to the project team. BOA also offers standalone inspections. Availability and scope depend on the product, factory access, inspection location, sampling or tests, and timing. Contact BOA to discuss your inspection needs or end-to-end support.

Protect intellectual property before sending production files, artwork, or tooling details to a factory. Start by listing the assets involved: product designs, technical specifications, trademarks, character artwork, packaging, moulds, and confidential manufacturing methods. Record who owns each asset and what the supplier may use it for. For licensed merchandise, share only approved artwork versions and define who can access them.
Protection needs to reflect the countries involved. Companies manufacturing and selling overseas should consider trademark registration in the relevant manufacturing and sales countries. Patent and design-right strategies may also cover the manufacturing country and the United States. Because these rights differ by jurisdiction, map where production will take place, where products will be sold, and which designs or marks need protection before releasing files.
Use a written agreement that addresses confidentiality, permitted use, ownership, subcontracting, tooling, and what happens when production ends. An NNN agreement covers non-disclosure, non-use, and non-circumvention. Draft it for enforceability in the country where manufacturing takes place, rather than copying it unchanged from another jurisdiction. If a factory uses subcontractors, contract terms should address their access to confidential materials and require appropriate protections.
Make the production contract specific. Identify the product, approved specifications, artwork revisions, tooling ownership, and restrictions on making extra units or selling project materials to other buyers. Define who may approve design changes and how unused files, samples, and tooling will be handled when production ends. Clear provisions reduce ambiguity, but they do not replace registration or physical controls.
Limit exposure across the supply chain. A project manager can give each factory only the files needed for its assigned production stage, restrict access to working files, and maintain a record of approved revisions. For example, a packaging supplier may need final box artwork but not the complete character model or product engineering files. If production is divided across suppliers, separate components or process stages so one supplier does not automatically receive the full product design. This can reduce information exposure, but adds coordination and quality-control demands.
Physical controls matter too. Use controlled access to sample rooms, tooling, and production files, and document who receives prototypes or artwork. Mark confidential drawings and sample records with project identifiers and revision status. For a collectible figurine, the approved sculpt, paint references, and licensed character artwork should have clear access permissions and release records. These controls help distinguish authorized production from unapproved copying.
Build safeguards into supplier onboarding and production changes. Before a new factory or subcontractor receives files, confirm the applicable agreement, asset ownership, permitted purpose, and access scope. When a design revision is approved, replace obsolete files and record which production batch uses the new version. This creates a traceable link between intellectual property, specifications, and manufacturing activity.
Labor rates matter, but they do not show what it costs to deliver acceptable products. Compare production productivity, reject rates, assembly requirements, factory capacity, and management effort alongside labor. This makes the comparison useful when deciding how to manage overseas manufacturing projects, instead of letting a headline wage figure determine the sourcing strategy.
Start with a shared production baseline. Use the same design revision, material, finish, order quantity, packaging, and acceptance criteria for each location. Then compare labor hours per completed unit and the amount of rework needed. A lower hourly rate may not reduce the cost per acceptable unit if the process requires extra handling or correction.
Tooling and setup also affect the comparison. A process with higher initial tooling costs may make sense at larger volumes, while a manual process may avoid that setup but require more labor per unit. Model the expected order quantity and plausible volume changes. For a product with several assembled parts, include the time and quality impact of sorting, assembly, and final packing.
How can a sourcing partner help companies compare overseas manufacturing with domestic or nearshore production? A partner aligns quotes and operating assumptions, then evaluates process fit, productivity, production capacity, oversight, and delivery requirements. This gives decision-makers a comparable view of each option, including how supplier capability and management needs affect the economics.
To manage overseas manufacturing projects effectively, compare more than one production scenario. A professional assesses:
• Labor hours and output per production shift, rather than wage rates alone.
• Tooling and setup against expected volume and possible design revisions.
• Yield, rework, and inspection findings in relation to sellable output.
• Transport, customs, and delivery requirements for the target market.
• Inventory timing, replenishment flexibility, and the cost of holding stock.
Use sensitivity analysis to show which assumptions drive the result. For example, compare the planned order with a lower-volume scenario, or model a design change that affects tooling or assembly. Keep quoted costs distinct from estimates, and record how different production yields or delivery arrangements change the cost per acceptable unit. This makes trade-offs visible without treating a forecast as a guaranteed outcome.
The final comparison should state the assumptions, delivery point, and decision criteria behind the recommendation. It should also show what would prompt a review, such as a specification revision, supplier capacity change, or new destination market. Discuss a landed-cost comparison for your manufacturing project.
Buying Office Asia connects supplier selection, factory-direct price negotiations, and production decisions within one sourcing plan. Its End-to-End Sourcing & Procurement support is useful when you need coordinated oversight across supplier evaluation, manufacturing, and cost planning rather than disconnected decisions at each stage. For larger production needs, high-volume sourcing and procurement can support a structured approach to supplier capacity and project requirements. A Dedicated Asia Procurement Team provides regional coordination as specifications, quotations, and production plans develop.
Bring your product requirements, target market, order expectations, and delivery priorities into the discussion. That gives the team a basis for aligning sourcing decisions with quality and financial objectives. If you’re planning overseas production, contact Buying Office Asia to discuss your project.
Your first production run can provide a stronger basis for future decisions. Use its records to track supplier responsiveness, recurring production issues, change control, and delivery performance. Then turn those findings into clearer specifications and more focused supplier development before the next order. This creates a working knowledge base that stays with your business as products and supply needs evolve.
A practical approach to managing overseas manufacturing projects treats supplier relationships as an ongoing operating capability, not a one-off transaction. Buying Office Asia supports this work through End-to-End Sourcing & Procurement, high-volume sourcing and procurement, and a Dedicated Asia Procurement Team. The right level of involvement depends on your production needs and the coordination your internal team requires.
Bring your next manufacturing decision into focus with a partner that can support the work beyond the initial sourcing choice. Discuss your manufacturing plans with Buying Office Asia, and take the next step with a clearer basis for growth.
Overseas manufacturing can provide access to specialized suppliers, production capacity, and materials that may not suit domestic sourcing. The trade-off is greater coordination across distance, language, transport, and time zones. A business launching a seasonal product, for example, should consider how a delayed shipment affects its selling window, not just the factory’s production capability. Diversifying suppliers or planning alternate production routes can reduce exposure to a single disruption.
Direct factory contact can work when your team can manage technical communication, supplier follow-up, and production decisions across the manufacturing location. An agent may coordinate commercial communication, but that role can differ from operational project management. Clarify who handles specification changes, production milestones, quality issues, and escalation. For example, if an artwork revision arrives during production, identify who communicates the approved file and records which batch uses it.
A professional weighs product complexity, expected volume, manufacturing process, supplier capability, destination requirements, and the time available for production and delivery. These variables interact. A component with tight tolerances may narrow the suitable factory options, while an uncertain forecast can make a large minimum order risky. A useful comparison tests how each supplier handles the product’s most demanding process, not just whether it can produce a similar category.
A local partner can provide ongoing operational coordination at the manufacturing location, while a trading agent may primarily connect buyer and seller and manage commercial communication. The distinction matters when a project needs factory follow-up, technical clarification, or escalation of a production issue. Define responsibilities in writing, including who tracks open actions, records decisions, and reports delays. This makes accountability clear without relying on job titles alone.
Establish decision owners and approval gates before production begins. The sequence usually moves from requirements and supplier assessment to quotation alignment, sample approval, production release, progress monitoring, inspection, and shipment readiness. A project tracker should capture each deliverable, its owner, due point, and approval status. That record helps distinguish a factory delay from a late design decision or unresolved packaging specification.
Agreements should define product scope, payment terms, acceptance criteria, confidentiality, intellectual property ownership, tooling control, subcontracting, change approval, and termination arrangements. Protection should reflect the manufacturing and sales countries involved. For example, a contract can limit a supplier’s use of licensed artwork to the approved production purpose and require controlled handling of design files. Registration strategies and contract terms vary by jurisdiction and asset type.
They affect the cost and release of imported goods through product classification, country of origin, customs value, required documents, and importer responsibilities. These details should match the actual product and transaction. A sourcing comparison should identify who supplies each document and handles each import obligation. Tariff exposure can change, so review the assumptions behind a cost estimate when the product, origin, destination, or applicable tariff schedule changes.
A sourcing partner can align factory completion, packaging details, shipment documentation, transport arrangements, and receiving requirements. Carton dimensions and gross weights help inform freight planning, while clear shipment milestones help warehouse teams prepare for arrival. Inventory planning should account for demand variability and replenishment lead time. Splitting an order across shipments may improve availability, but can add handling and coordination, so include that trade-off in the delivery plan.
The biggest risk in contract manufacturing in India is not simply finding a factory. It is starting production before product specifications, responsibilities and intellectual property terms are clearly documented.Finding and contacting suitable manufacturers is an important first step, but the righ...
A manufacturer’s quotation can look right while the factory behind it lacks the capacity or quality controls your product needs. Knowing how to vet manufacturing suppliers in Asia means assessing production fit, business credentials, quality practices, and sample results before committing to an orde...
A Certificate of Origin can affect how customs assesses a shipment at its destination, so accurate origin information matters. If you’re asking what a certificate of origin is, it’s a document declaring the country where goods were manufactured, produced or last substantially transformed. It may sup...